Buyer guide
How Pickleball Paddles Are Made: Buyer Questions
Use the pickleball paddle manufacturing process as a sequence of purchasing checkpoints. Each stage should produce information that helps you approve the next step.
Last updated
How pickleball paddles are made: the short version
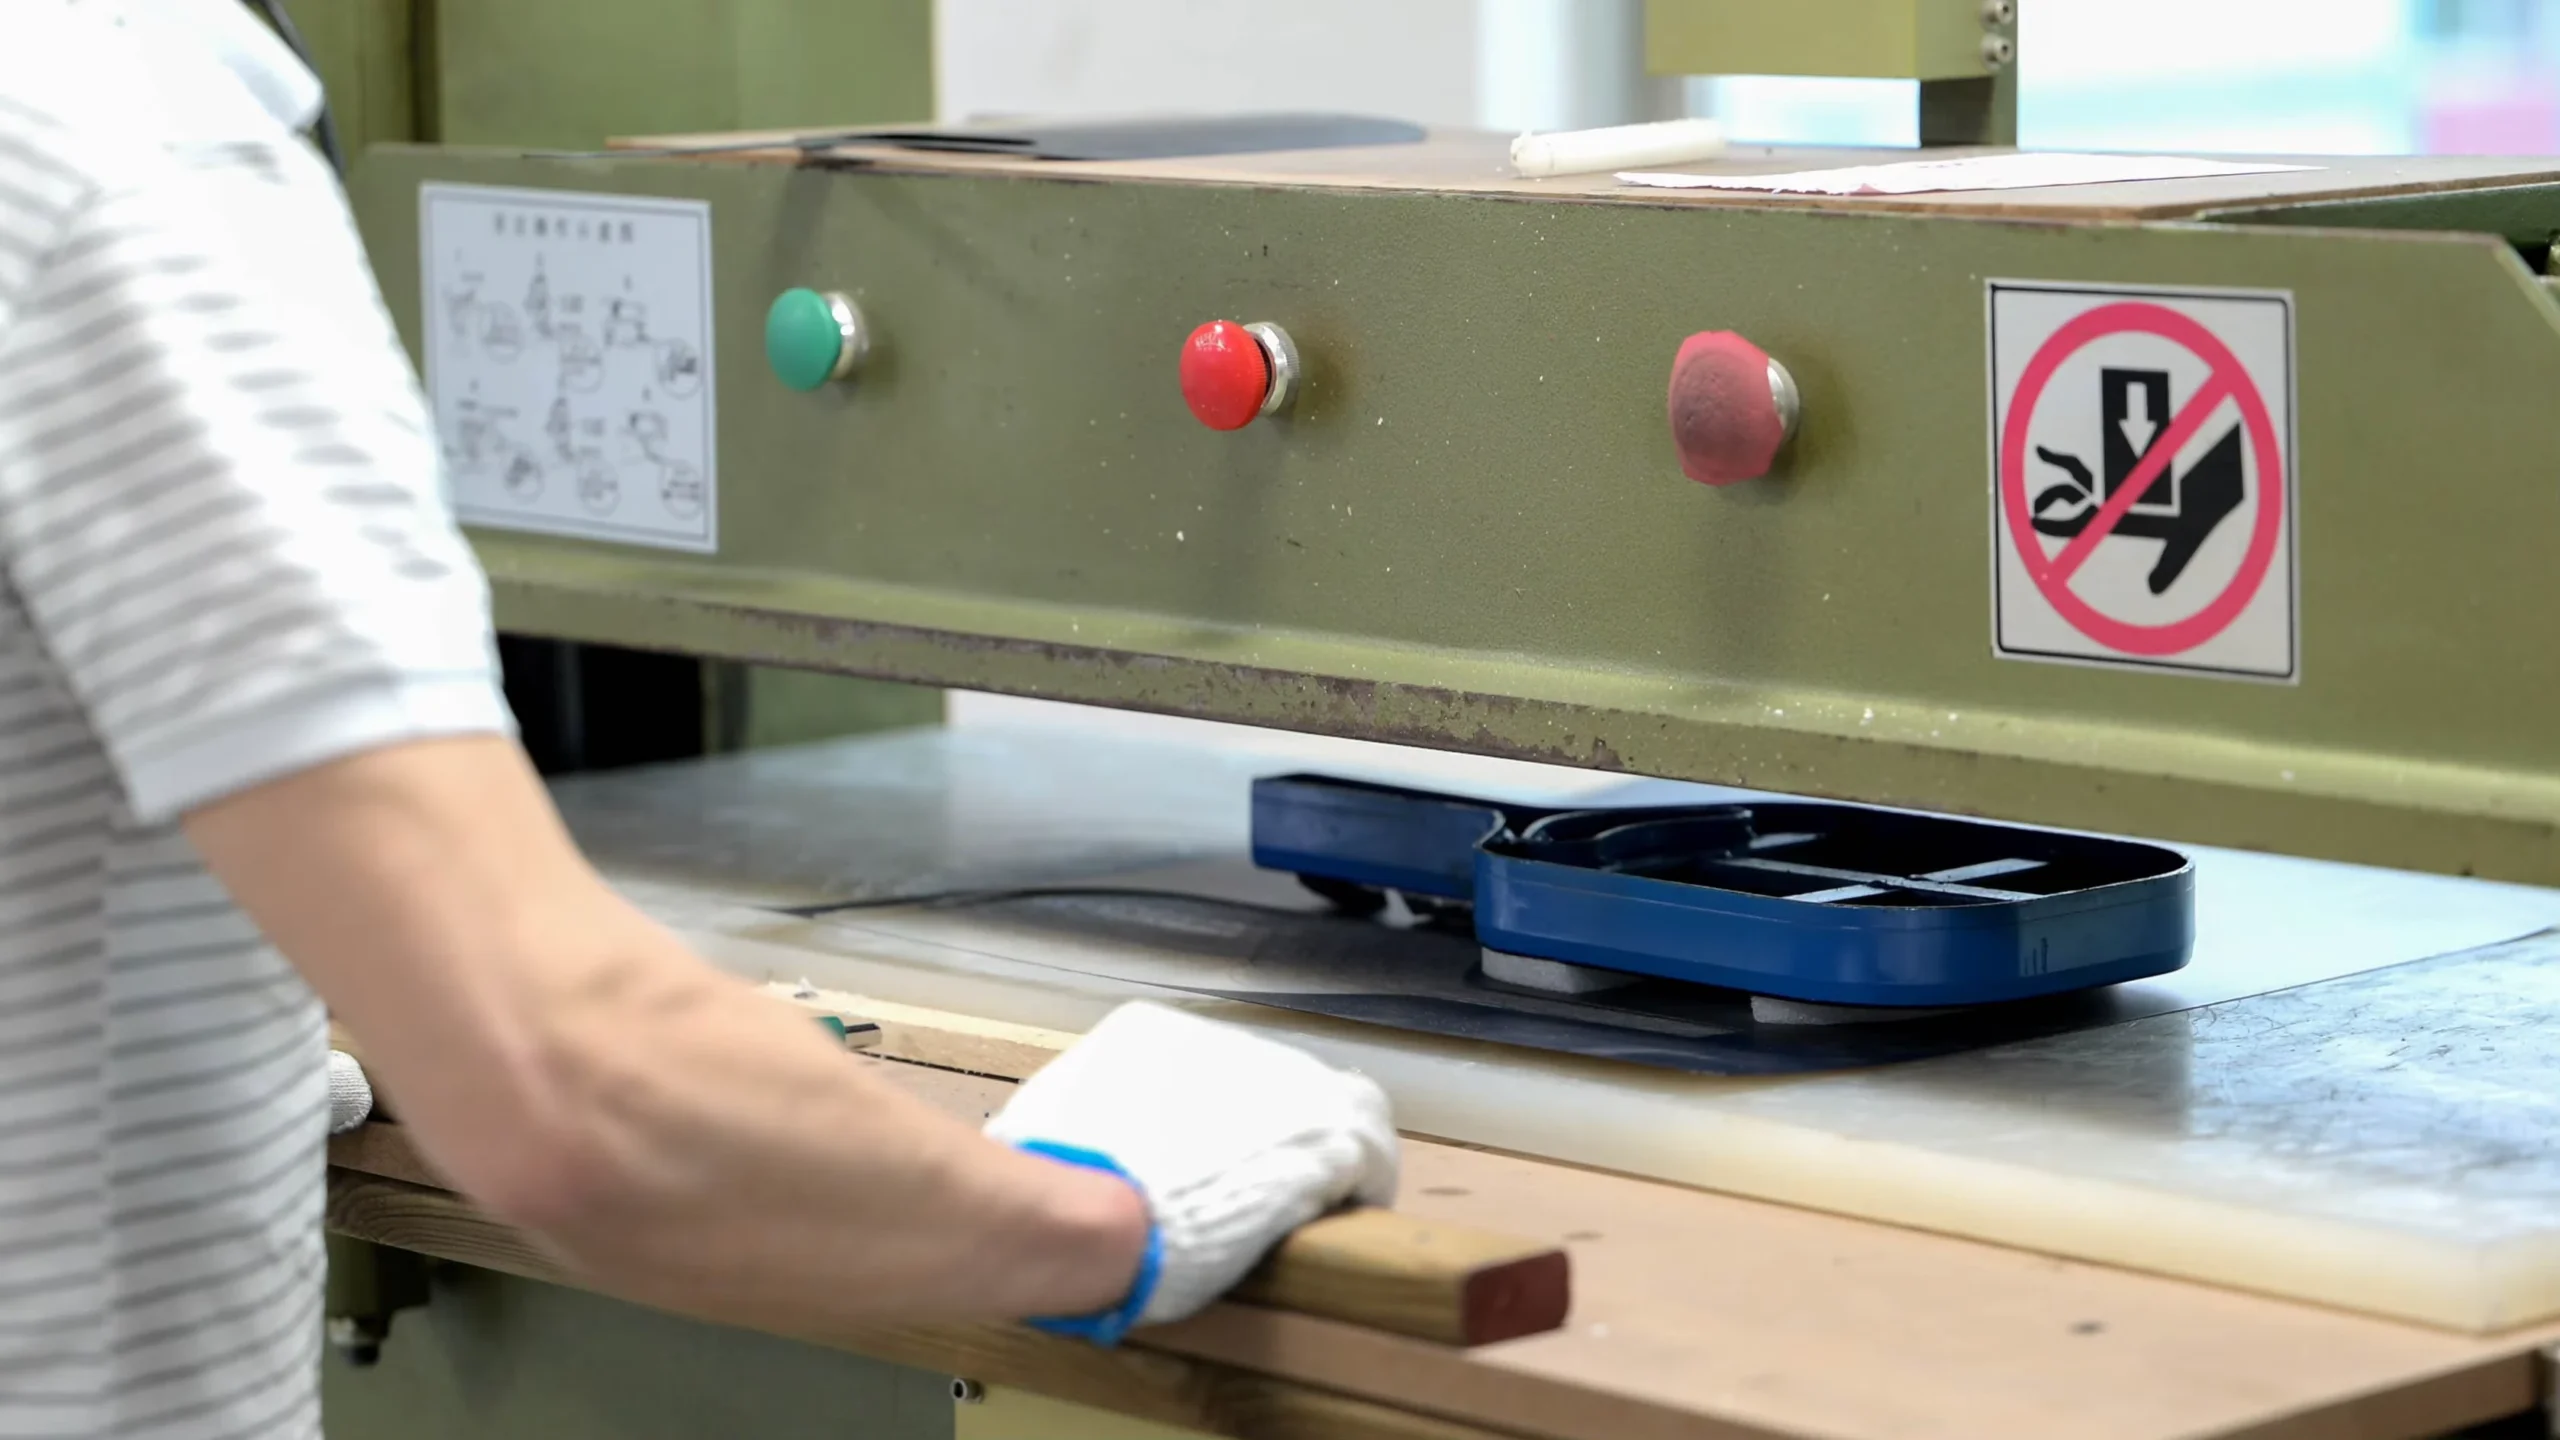
Almost every paddle goes through the same stages: prepare the face skins, cut the core, bond faces and core under pressure, form the edge and handle, finish and print the surface, then inspect and pack. What differs between a value paddle and a performance paddle is mainly the bonding stage (cold or hot press), the materials and how tightly each step is controlled. This guide walks through the stages as a buyer, with the questions that tell you what you are actually getting. Our own sequence is described on our production workflow.
1. Face skins
The face is a thin composite sheet: fiberglass, carbon fiber (T300 and T700 grades, or woven 3K to 18K patterns), aramid, titanium-fiber or a hybrid. Carbon faces are built from several layers, and the angle of each layer (for example 0°, 45° and 90°) changes stiffness along and across the paddle. Some faces are textured during pressing; others get a printed or coated surface later.
Ask: which material and grade, how many layers, at which angles, and whether the texture is molded in or applied. See T700 carbon face architecture for how face architecture is modelled.
2. Core preparation
The core is cut to the outline from honeycomb or foam sheet, usually by CNC. Patterned foam cores (cells, grooves, gears or bridges) are machined or molded before assembly, and hybrid builds add foam strips at the perimeter.
Ask: core material, density or cell size, thickness, and whether the core runs into the handle. The core sourcing guide lists the questions in full.
3. Bonding faces and core
This is the stage that most separates paddle types.
- Cold press / cold-cut assembly. Faces are bonded to the core with adhesive at room temperature under pressure. It is fast and economical, which is why it is used for entry-level and promotional paddles. Our JT-1 carbon, fiberglass, junior and mini paddles use this route.
- Hot press (thermoforming). Face, resin and core are cured together under heat and pressure in a closed mould. The bond is stronger and the structure more uniform; many hot-pressed paddles are "unibody" builds with a sealed edge. It costs more and takes longer per cycle. Our thermoformed paddle page explains the term.
- Semi-hot press. Our name for a route between the two, used on many of our carbon and foam performance models. See the semi-hot-press reference for how we treat it in modelling.
Ask: which route, and what cure temperature, pressure and time records exist for your batch.
4. Edge, handle and grip
After pressing, the blank is trimmed. The edge is either sealed with an edge guard (a plastic or rubber channel bonded around the perimeter) or finished edgeless on some hot-pressed builds. The handle is built up to the specified length and shape, then wrapped with a cushion grip; a butt cap closes the end and often carries a logo.
Ask: edge guard material and colour, handle length and shape, grip type and circumference, and what the butt cap shows. These details change weight and balance, so they belong in the specification.
5. Surface finishing and print
Artwork is applied by UV printing or water-transfer printing, then protected where needed. A textured face may be molded, sprayed or left as the raw weave. Gloss-varnished edge guards and coloured grips are added at this stage.
Ask: print method for each design, how colours are matched, and whether the surface texture is part of the face or a coating. USA Pickleball tests surface roughness, so the method matters if you plan to apply for approval (see compliance and evidence).
6. Inspection and packing
Finished paddles are checked for dimensions, weight, appearance and bond defects, then packed with their accessories. Good practice is to weigh every paddle and record the batch distribution, and to keep one approved sample as the reference.
Ask: which checks are 100% and which are sampled, the weight tolerance, and what you receive as a record. Many buyers also book an independent pre-shipment inspection using an AQL sampling plan; our quality and acceptance planning page explains how to set acceptance criteria.
What drives the price of a paddle
Most of the price difference between paddles comes from a handful of choices made in the stages above.
| Choice | Lower cost | Higher cost |
|---|---|---|
| Face | Fiberglass, smooth T300 carbon | T700, 3D 18K, aramid or titanium-fiber faces |
| Core | Plain PP honeycomb | Patterned, bridged or full foam cores |
| Process | Cold press or cold-cut assembly | Hot press, with longer cycle times |
| Outline | An existing mold | A new custom mold |
| Artwork | One design, few colours | Many designs, two-sided print, special finishes |
| Packing | Polybag or simple box | Book-style or magnetic box with accessories |
Quantity matters too: setup work for each design is spread over the run, so price breaks usually come with quantity per design.
Common defects and where they come from
- Delamination or a hollow sound: a weak bond between face and core, usually from the pressing stage. Tap-test samples and ask how bond quality is checked.
- Dead spots: local core damage, often crushed honeycomb cells. Check sound and feel across the face on samples.
- Edge guard lifting: adhesive or fit problems at the edge. Inspect the joint, especially at the throat.
- Weight spread: variation in core density, resin or grip build-up. Ask for the batch weight distribution, not only the average.
- Print faults: misregistration, colour shift or scratches. Approve printed samples for every design.
Write the defects that matter to you into the acceptance criteria, with the approved sample as the reference.
Buyer checkpoints by stage
| Stage | Confirm before it starts | Record you should get |
|---|---|---|
| Materials | Face grade and layers, core and density, outline and thickness | Specification revision |
| Sample | Edge, handle, grip, print method, weight target | Measured sample sheet and approved photos |
| Production | Approved sample, tolerances, changes allowed | Batch weight distribution and inspection notes |
| Dispatch | Packing list, carton marks, accessories | Packing list, inspection report, shipping documents |
Frequently asked questions
How are pickleball paddles made?
Face skins and a honeycomb or foam core are cut to shape, bonded under pressure (cold or hot), trimmed, fitted with an edge guard and handle, printed, inspected and packed.
What is the difference between cold-pressed and hot-pressed paddles?
Cold pressing bonds the faces with adhesive at room temperature and is faster and cheaper. Hot pressing cures face, resin and core together under heat, giving a stronger, more uniform bond at a higher cost.
What is a thermoformed pickleball paddle?
A paddle whose face and core are cured together under heat and pressure, often as a sealed unibody shell. It is another name for a hot-pressed build.
How long does it take to make pickleball paddles?
It depends on the build, quantity and artwork. Sampling and production times are confirmed in each quotation.